Technical Capabilities
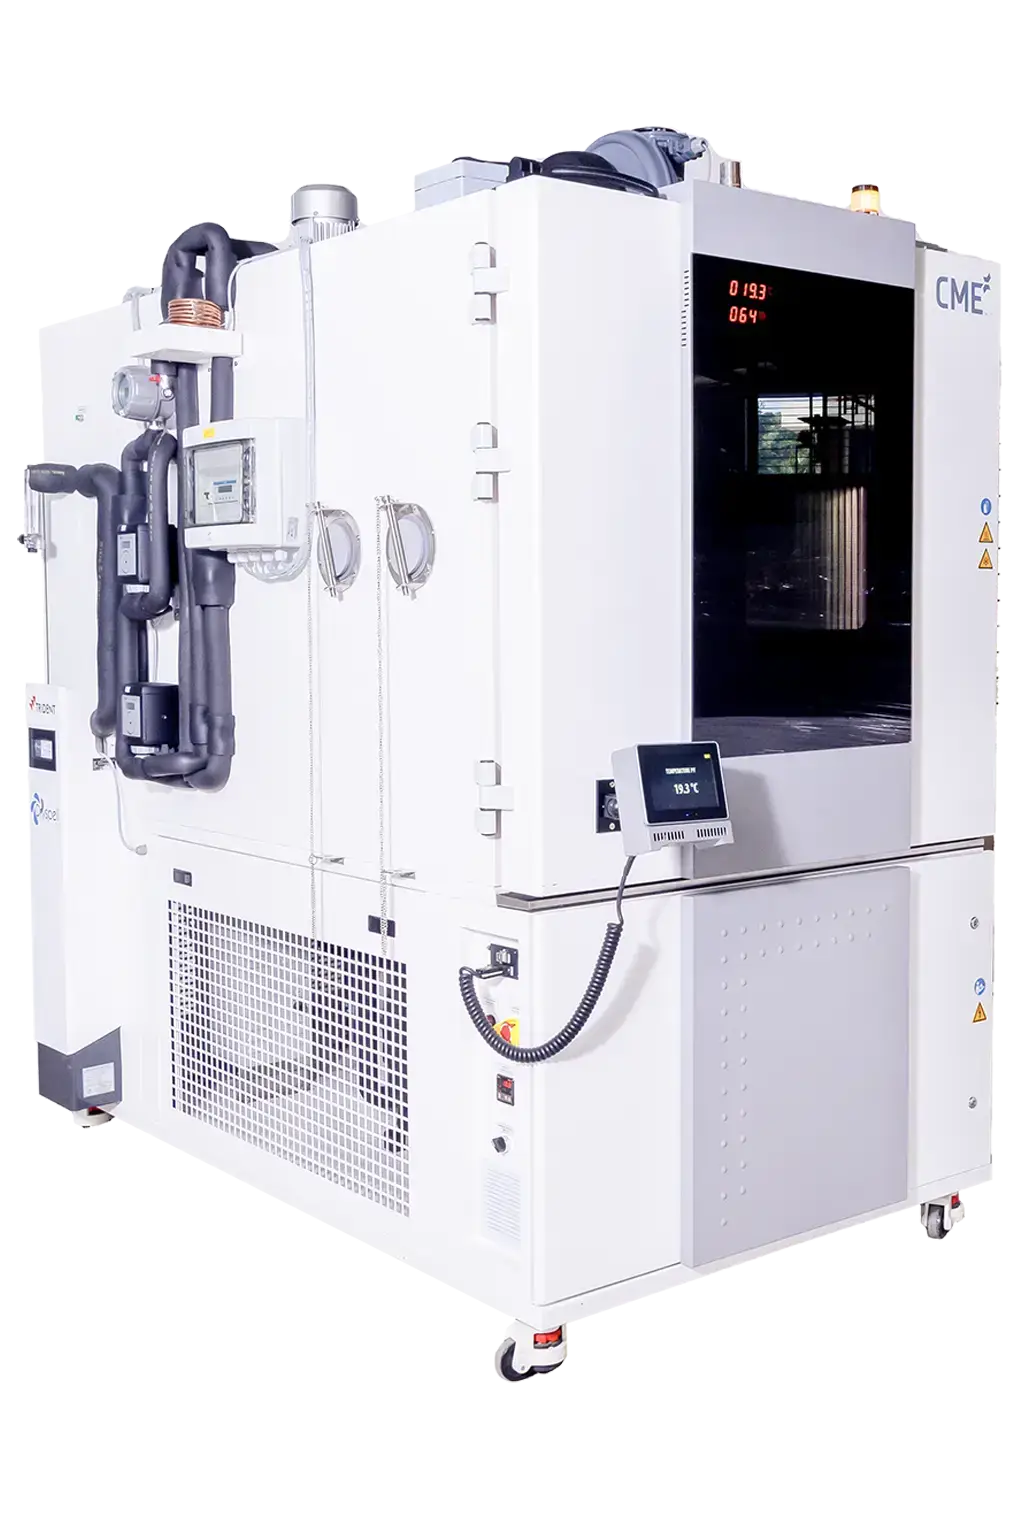
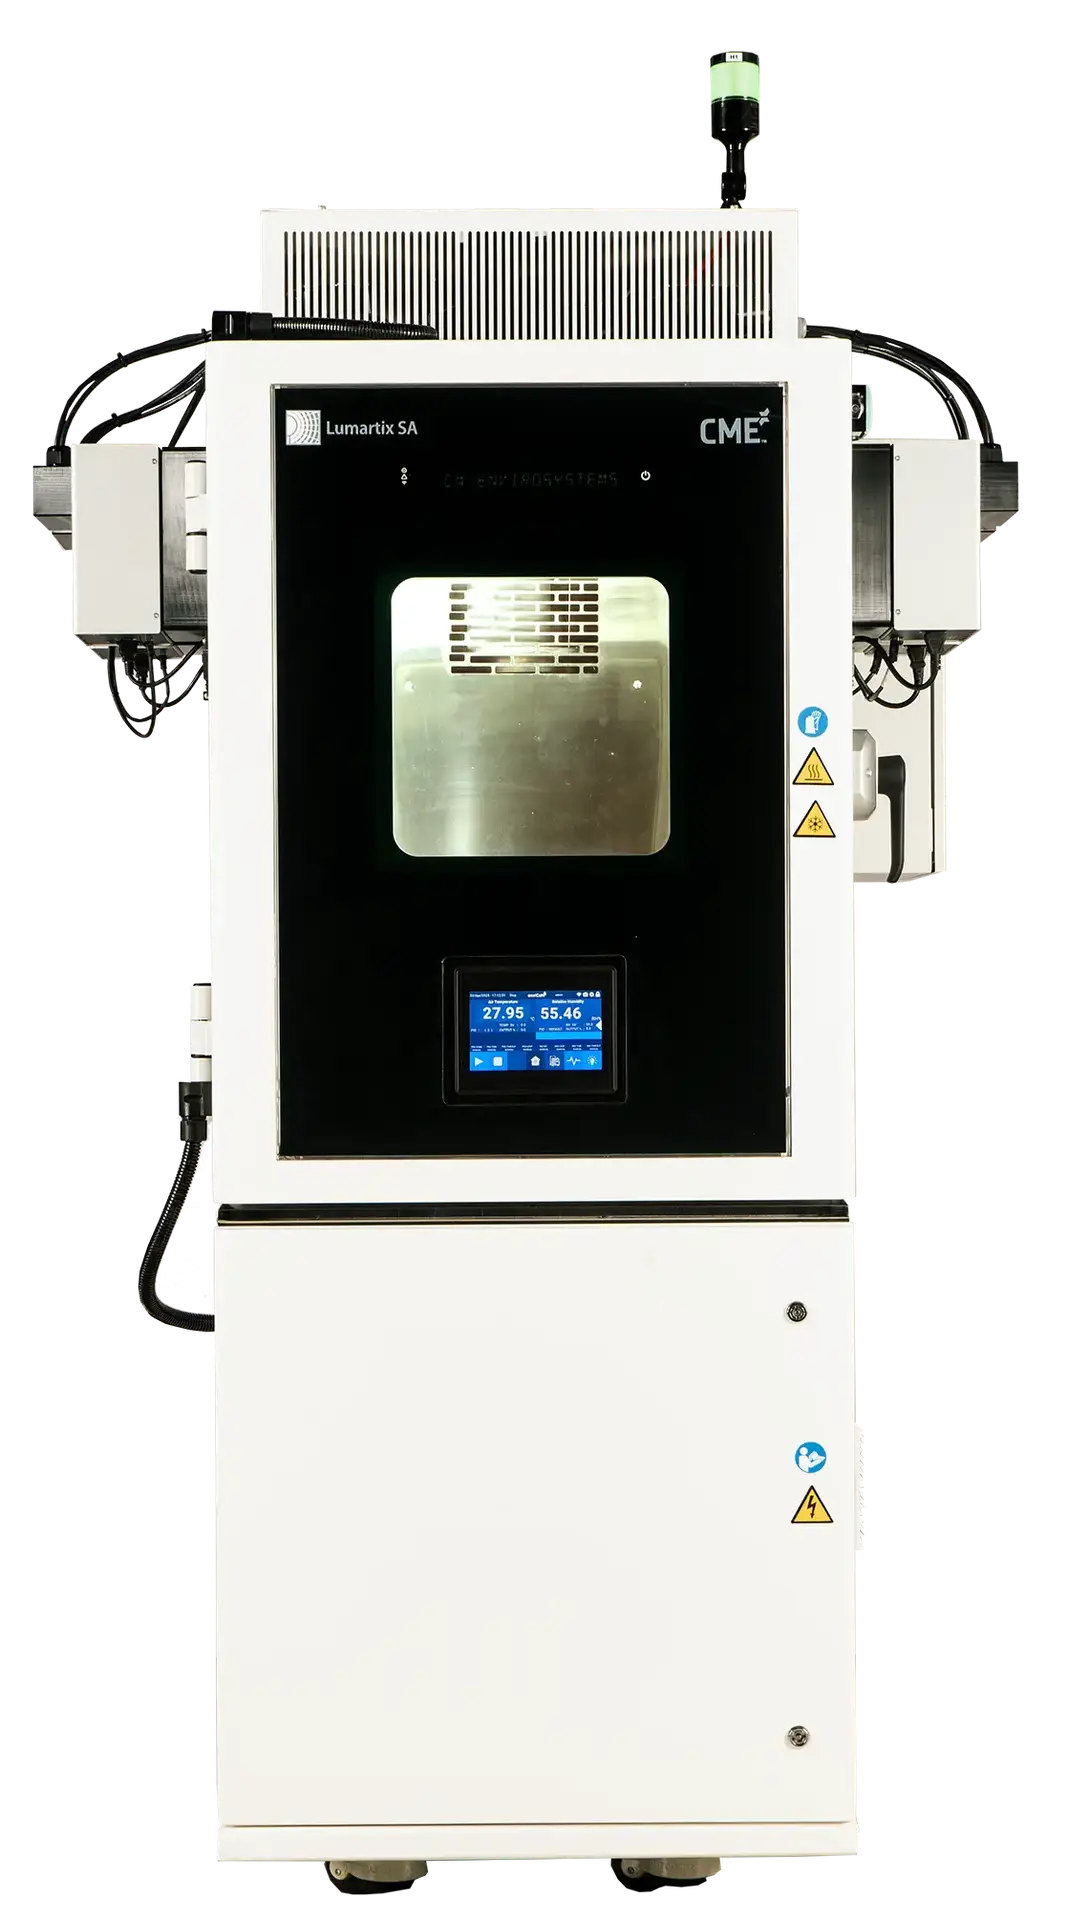
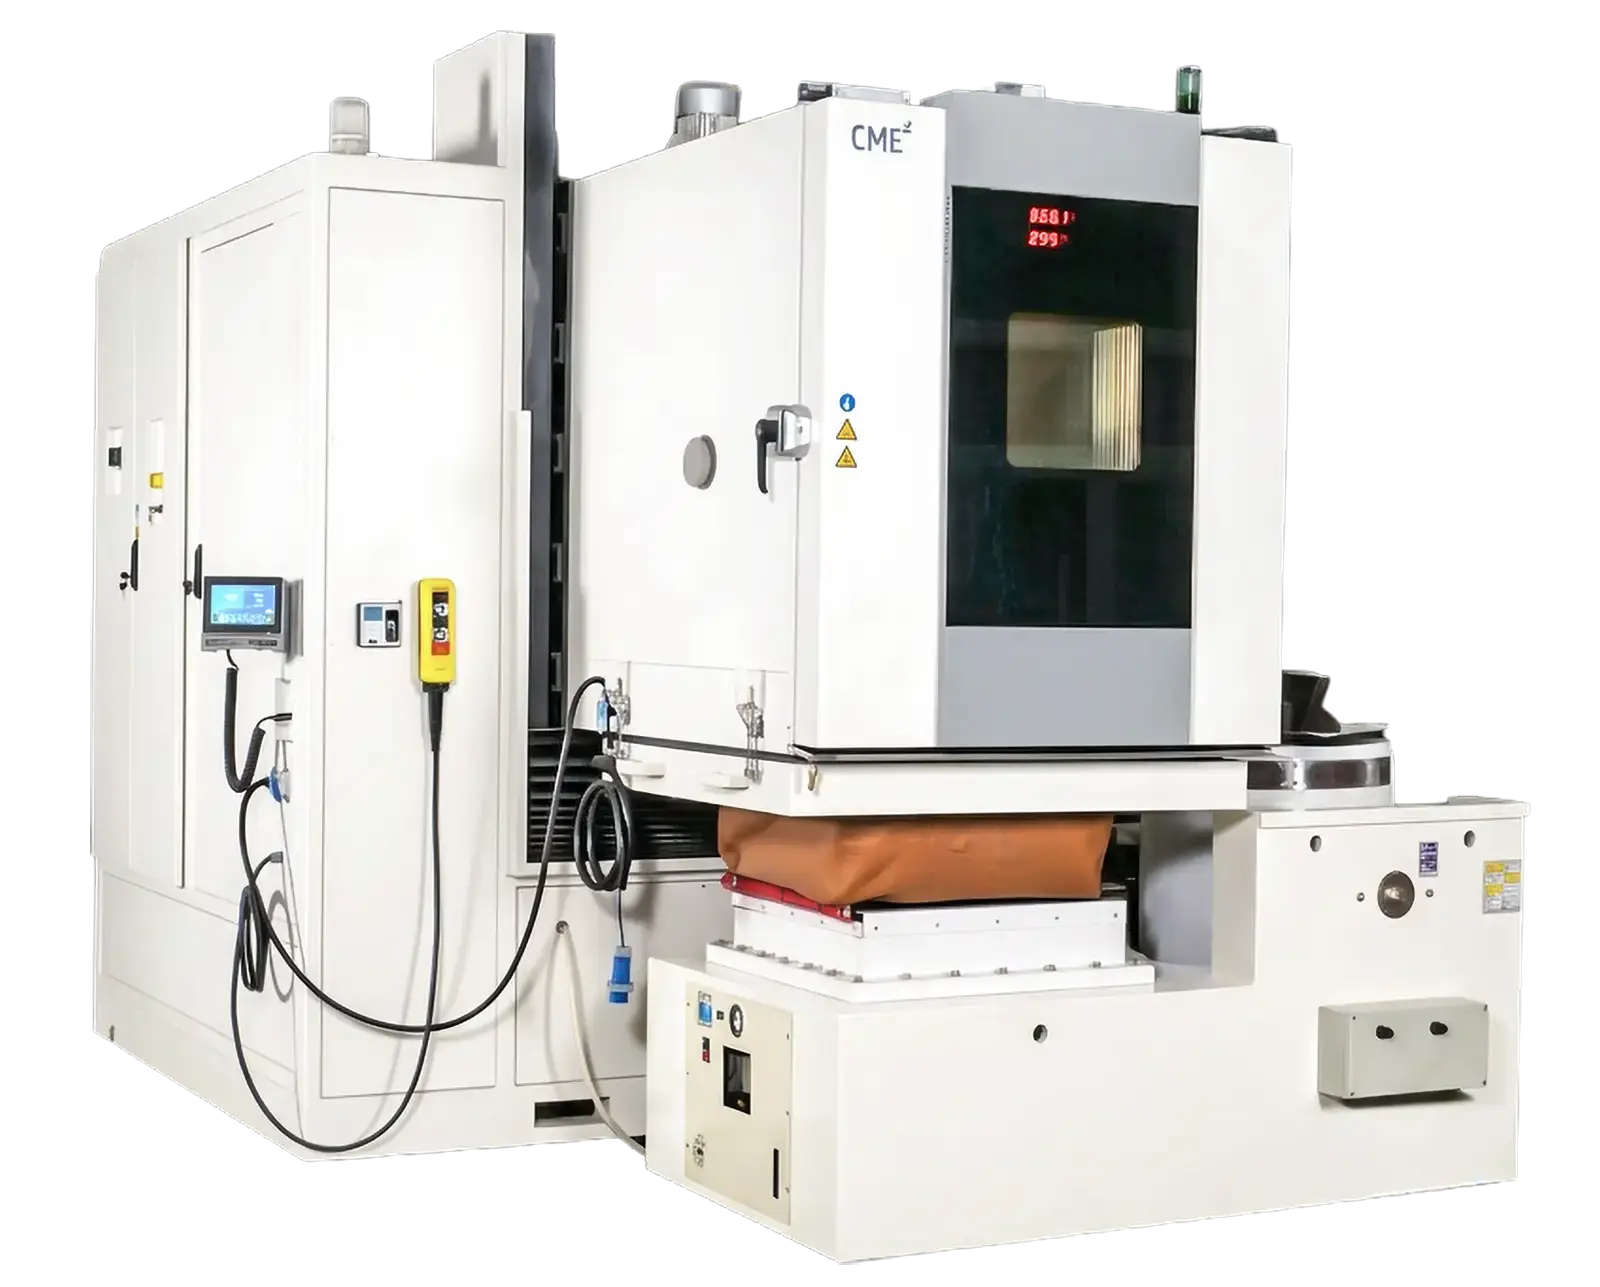
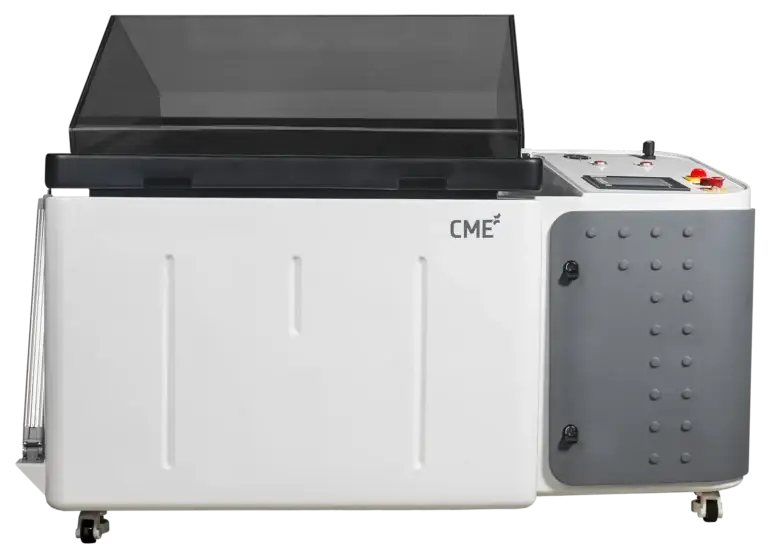
Our testing solutions leverage precise mechanical, electrical, and thermal architectures. Please note: The implementation of specific subsystems and overall technical integration depend entirely on your designated chamber classification and custom parameter requirements.
Single or robust cascade refrigeration configurations featuring eco-friendly low-GWP refrigerants, custom thermal expansion loops, and continuous pressure modulating hardware.
Low-watt density open nichrome wire elements coupled with rapid solid-state switching (SSR). Provides quick thermal ramp rates without causing temperature overshoot.
Self-contained steam generator vapor systems, demineralized water distribution pathways, and high-efficiency mechanical or desiccant air dehumidification.
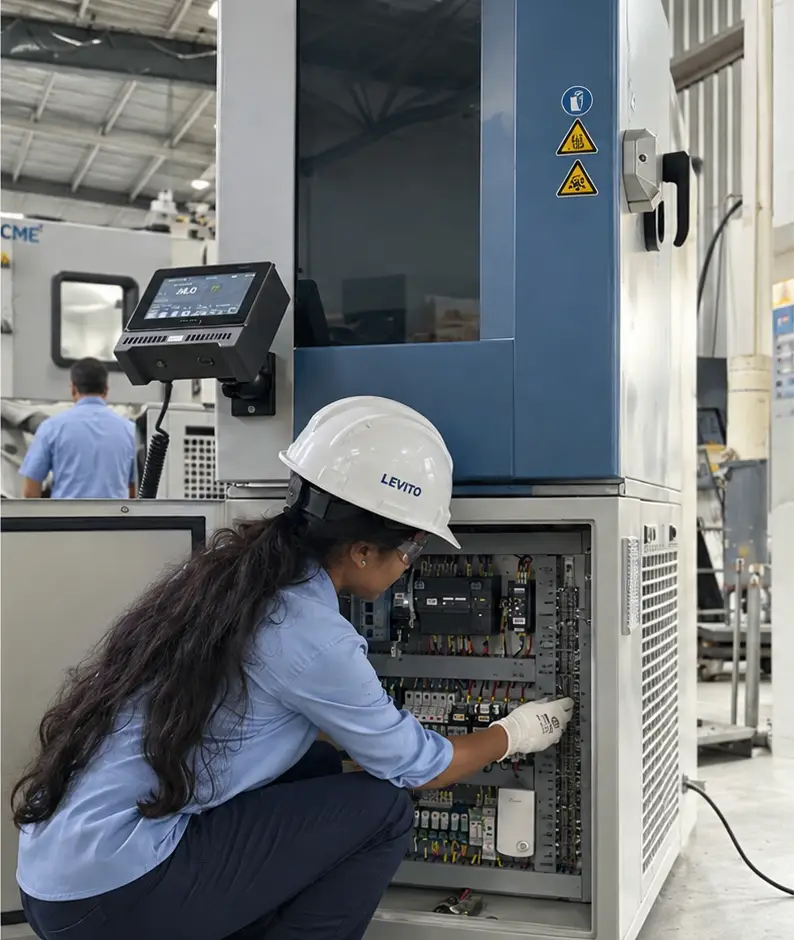
UL 508A compliant electrical assemblies. Built with integrated overcurrent devices, branch circuit protection, noise filtration, and clean logic wiring corridors.
Advanced controller units offering dual PID auto-tuning loops, secure Ethernet connectivity, on-board data logging, and seamless standard SCADA integration.
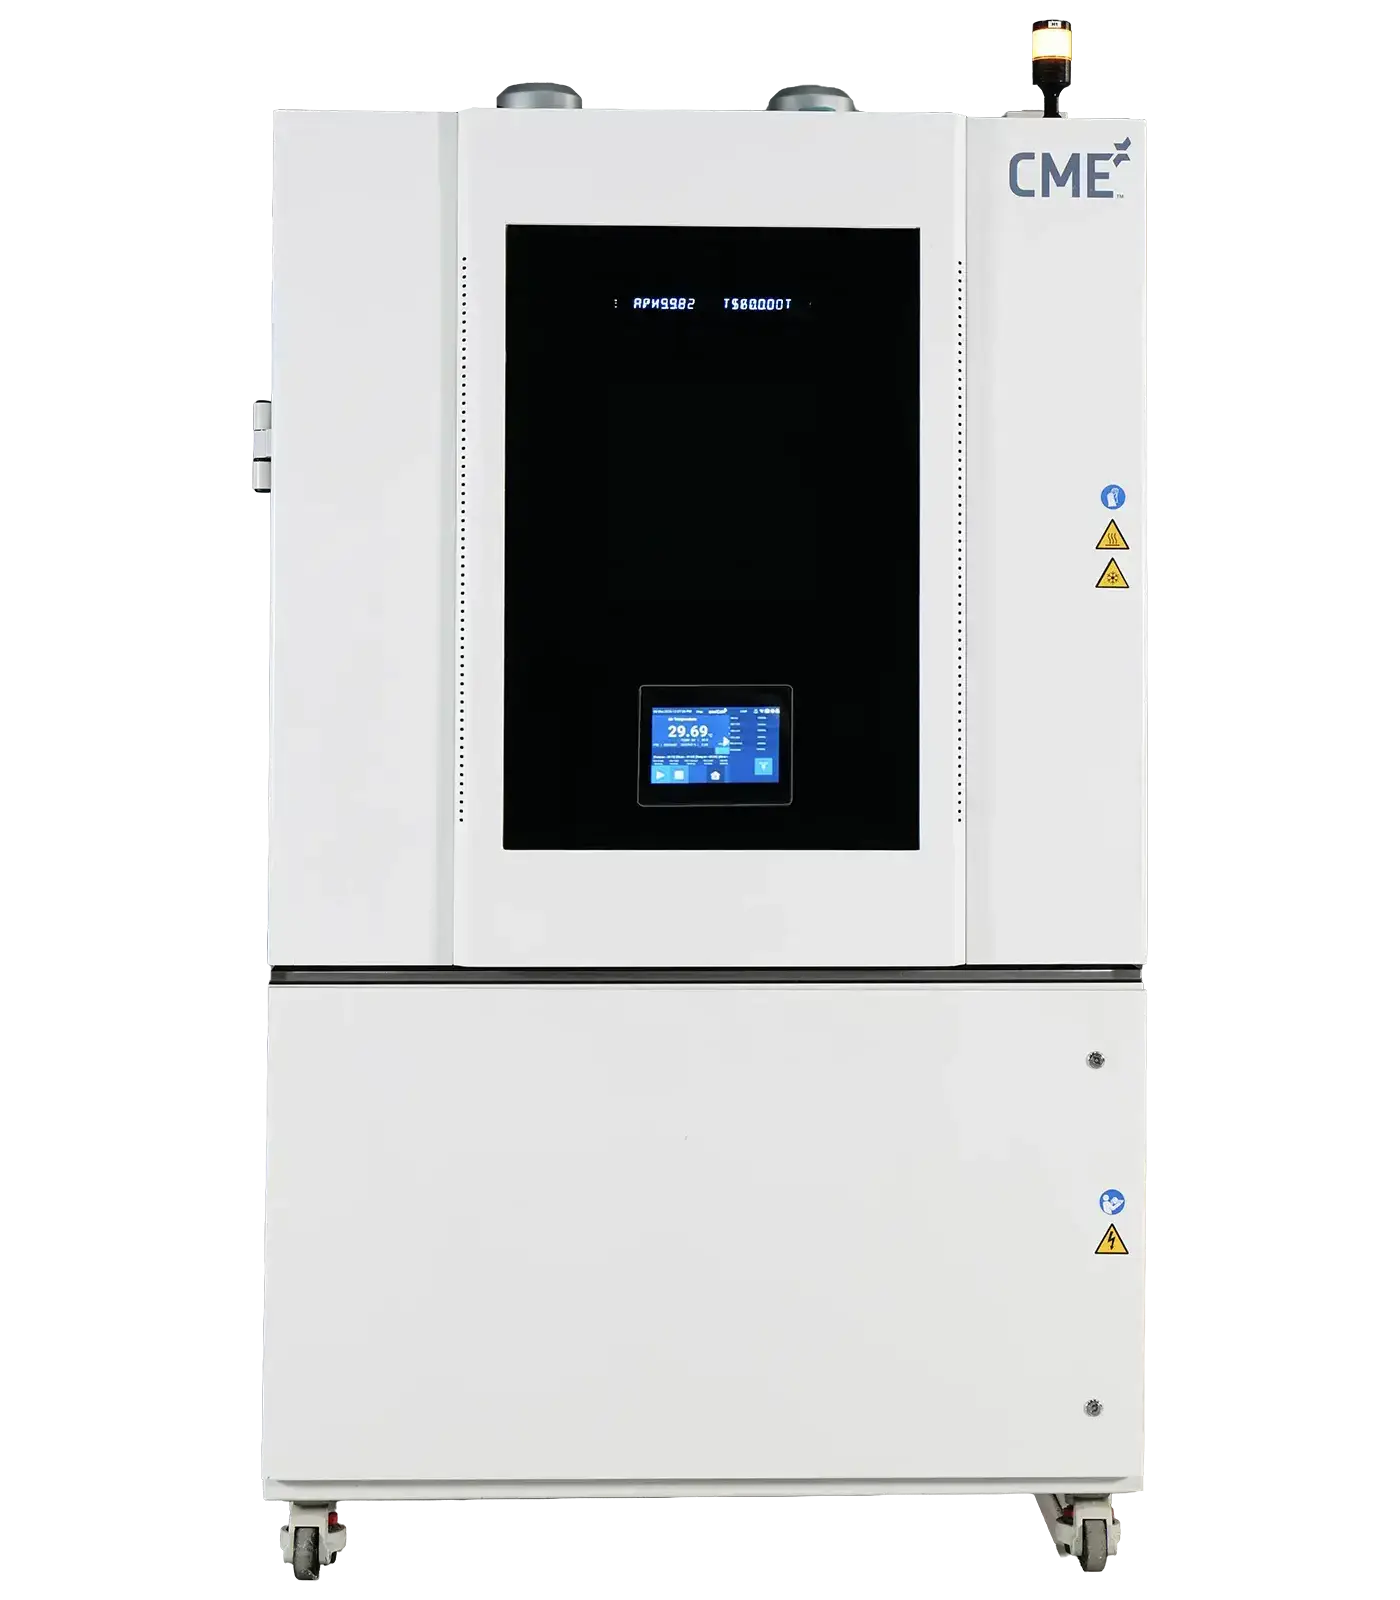
Industrial PLCs equipped with responsive color touchscreens, flexible recipe editors, comprehensive audit trails, and multi-tier user access permissions.
Highly stable Pt100 RTDs and capacitive relative humidity sensors calibrated to NIST standards, maintaining tight accuracy margins over wide operational ranges.
Dynamically balanced stainless steel conditioning blower fans driven by heavy-duty external motors. Delivers uniform laminar airflow profiles across all sample shelves.
Double-wall 304 stainless steel interior liners, reinforced base floors for heavy payloads, non-settling fiberglass wool insulation, and positive pressure latch handles.
Redundant physical high-temperature switches, low-water cutoff circuitry, automatic refrigerant pressure relief ports, and flashing beacon status alarms.